
Laser Welder vs MIG: The Honest, Scene-by-Scene Guide
A few months ago, someone on r/Welding asked the question behind every laser welder vs MIG debate:
“Never welded before, would have no idea how to TIG/MIG. I need to restore a car — mostly floor pans. If money wasn’t an issue, would you buy a new MIG welder, or just go with a laser welder and try out the next-gen stuff right from the beginning?”
The poster was a weekend hobbyist with zero welding experience. But the question underneath his post — should I buy a laser, or stick with a traditional welder? — is the same question a production manager asks before committing real money to new equipment. His intuition was reasonable: lasers are newer, cleaner, more “high-tech” — so they must be easier and better, right?
The community disagreed. Almost unanimously.
A quick disclosure before we go further: we make laser welders. So when this guide says a laser is the wrong tool for a job, it isn’t a sales pitch — it costs us a sale to say so. That’s exactly why the next part matters.
Of the 76 replies, nearly every one told him to buy a MIG. The highest-rated comments came from people who operate laser systems professionally — and they were the loudest voices against it.
Here’s the part that surprises most people: the pros weren’t against lasers. They were against a laser in that situation.
That distinction is the entire point of this guide. The real question isn’t “which is better.” It’s “which fits your scene.”
Here’s what this guide covers: the question that started it all, why the pros pushed back, and the scene-by-scene boundary between MIG and laser — so you can decide which fits yours.
The Reddit Question That Started It All
The post captured a common misunderstanding in three sentences:
- The poster had never welded anything.
- He wanted to repair thin, rusty, greasy sheet metal on an old car.
- He assumed a laser welder would be the easier, more advanced choice.
That assumption — “newer technology = simpler to use” — is where most buyers go wrong. It’s not a beginner’s mistake. It’s a category mistake.
A laser welder is not a better MIG. It’s a different tool, built for a different job.
Why the Pros All Said "No"
The top comments from r/Welding read like a safety briefing. A few stand out:
“A laser can literally blind someone if you are careless with it.”
“These devices can ignite things from 10–15 metres away. And reflections can ignite at close range.”
“Adjusting the laser is extremely difficult. The ease of the laser is replaced by the dangers.”
“These shouldn’t be in the hands of amateurs and inexperienced.”
One reply came from a user who has operated fiber laser systems up to 10 kW. His summary was blunt: a laser “projects pure heat” — it can and will ignite anything that can ignite.
Reading those, you’d think lasers are a terrible technology. They’re not. Those warnings are all true, and all of them point to the same conclusion: the problem wasn’t the laser. It was the use case.
A beginner repairing thin, dirty car panels in a home garage is exactly the wrong scene for a laser. That doesn’t make lasers bad. It makes the match wrong.
The Real Question Isn't "Which Is Better"
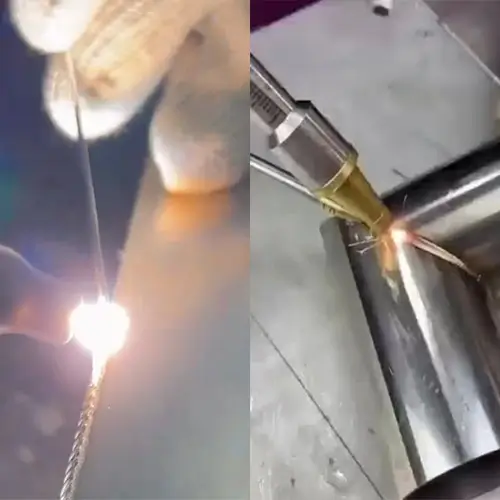
Ask a carpenter whether a hammer or a screwdriver is “better” and you’ll get the same answer every time: better for what?
The same applies here. The whole laser welder vs MIG debate usually frames the two as competitors — but they overlap less than most people assume. They’re built for different materials, different environments, and different production realities.
So instead of ranking them, let’s draw the boundary. Here’s where each one wins.
When MIG Wins
MIG (Metal Inert Gas) welding has been the workhorse of metal fabrication for decades — the process the American Welding Society still names first for automotive and structural work — and in several scenes it remains the correct answer.
1. Automotive body work and restoration. Old car panels are thin, rusty, warped, and full of small gaps where rust was cut out. Laser welding needs tight, clean fit-up — gaps that a MIG can bridge with filler wire become blow-through holes under a laser.
2. Dirty, uncontrolled environments. A laser is a precision optical instrument. Too much dust in the air can damage optics and burn out components. MIG is rugged and tolerates shop-floor reality.
3. Thick material and wide thickness ranges. MIG can weld from 26-gauge sheet up to 3/4-inch plate in a single pass depending on the machine. Laser struggles on thicker sections, and the power required to handle them drives the price up fast.
4. Gap-filling and imperfect fit-up. MIG feeds filler wire, which bridges small gaps and rebuilds joints. Laser welding is largely autogenous — no filler — so it demands near-perfect joint preparation.
5. Field work and portability. A MIG machine can be fixed on site by most welders and moved wherever it’s needed. A laser is more delicate and harder to service outside a controlled setting.
The community put it best: “MIG will always be baby’s first welder. If you can use a hot glue gun, you can use a MIG welder.”
When Laser Wins
Now the other side of the boundary — the scenes where a laser doesn’t just match MIG, it replaces it outright.
1. High-volume production. Laser welding is much faster on thin sheet metal — often two to four times faster than TIG on the same material. In a production line where the same weld repeats hundreds of times a day, that speed compounds into more finished parts per shift and a lower labor cost per part.
2. Thin stainless steel with zero distortion. This is the killer application. On 0.5–2 mm stainless steel, a laser’s concentrated heat input produces a narrow weld with almost no warping — and no black oxide, spatter, or the hours of grinding and polishing that a traditional weld leaves behind.
3. Precision and cosmetic welds. Lasers produce narrow, consistent, visually clean seams. For visible surfaces — kitchen equipment, cabinets, handrails, architectural metal — that means a finished weld straight off the machine, not one that needs post-processing.
4. Sanitary and medical-grade work. In food, pharmaceutical, and medical fabrication, the smooth, low-contamination weld a laser produces is a genuine process requirement, not a preference.
5. Labor economics. A laser doesn’t remove the operator — it amplifies them. An experienced welder can supervise a laser and produce at a rate that would otherwise demand two to three additional hands on grinders. In markets where skilled welders are scarce and expensive, that’s the difference between meeting a deadline and losing the order.
Notice what these scenes have in common: controlled environment, clean or well-fitted material, repetition, and a focus on speed and finish. That’s the laser’s home turf.
The Safety Truth
Laser safety deserves a section of its own, because it’s the biggest fear buyers bring to the table — and it’s worth separating fact from exaggeration.
What’s true: A fiber laser emits infrared light that can cause permanent eye damage instantly. Reflections can carry enough energy to ignite materials meters away. A beam that penetrates the workpiece can ignite whatever is behind it. None of this is theoretical.
What’s exaggerated: The danger is manageable with proper controls. OSHA’s laser hazard guidance comes down to the same basics: certified laser safety eyewear matched to the laser’s wavelength, a shielded or enclosed work area, and disciplined operating procedure. The horror stories almost always involve someone welding without eye protection, treating the tool like a toy, or disabling interlocks.
The honest takeaway: a laser is not more dangerous than any other industrial tool when handled correctly — but the consequences of carelessness are faster and more severe. That’s why laser welding belongs in the hands of trained operators and supervised production environments, not as a first machine for someone learning in a garage. If you can’t guarantee that environment — proper eyewear, a shielded work area, and trained operators — the honest advice is to hold off until you can. Reputable suppliers follow standards like ANSI Z136 for laser safety, and a serious shop should expect the same discipline from its operators.
Laser Welder vs MIG: Side-by-Side
To recap everything above, here’s the comparison at a glance:
| Dimension | MIG Welding | Laser Welding |
|---|---|---|
| Best material range | Thin sheet to thick plate (26ga–3/4") | Thin sheet, especially 0.5–2mm stainless/aluminum |
| Fit-up tolerance | Forgiving — filler wire bridges gaps | Demanding — needs tight, clean joints |
| Environment | Rugged, works in the field | Clean, controlled, low-dust |
| Operator skill floor | Low — beginner friendly | Higher — needs trained supervision |
| Post-weld finishing | Grinding/polishing often required | Minimal to none on thin material |
| Speed on thin sheet | Moderate | 2–4× faster than traditional welding |
| Typical buyer | Job shop, autobody, general fabrication | Production line, precision/kitchen/medical fab |
| Entry price | Low to moderate | High |
How to Choose: A Simple Decision Framework
Work through these five questions in order. By the end, the answer is usually obvious.
What are you welding?
Thin stainless or aluminum where distortion matters → lean laser.
Thick or mixed materials → MIG.
What's the environment?
Clean, controlled production floor → laser is viable.
Dirty shop or field work → MIG.
What's the volume?
Repetitive production at speed → laser pays for itself.
One-off or occasional repairs → MIG.
Who's operating it?
Trained operators in a supervised setting → laser.
General staff or a beginner → MIG.
What's the finish requirement?
Weld-and-done cosmetic seams → laser.
Welds that get ground or hidden anyway → MIG.
If you answered “laser” to most of these, you’re looking at a genuine production upgrade, not a novelty.
If you answered “MIG,” you’ve just saved yourself from an expensive mismatch.
If laser is your answer, the fastest way to confirm it is to test one on your own material — more on that below.
FAQ
Still weighing your options? Here are the questions buyers ask most often:
Generally no. Laser welding requires tight fit-up, strict safety discipline, and trained supervision. Most professionals recommend MIG as a first welding process because it’s more forgiving and safer to learn on.
It’s a poor fit. Old car panels are thin, rusty, and full of gaps. Laser welding needs clean, precisely fitted joints and will blow through imperfect sheet metal. MIG is the standard for autobody for good reason.
Reputable units are a serious capital investment — much more than an entry-level MIG. The gap narrows when you factor in the finishing labor a laser eliminates, but the upfront cost is real — which is why a serious supplier should help you model payback against your actual volume and labor rates before you buy.
It carries real hazards — eye damage from infrared light and fire risk from reflections. These are manageable with proper laser-rated eye protection, a controlled work area, and trained operators. The danger comes from carelessness, not from the technology itself.
Laser performance drops off on thicker material, and the power required to handle it becomes expensive. For thick sections(ie: thicker than 8mm), traditional processes like MIG remain more practical.
On thin sheet metal, laser welding is typically two to four times faster than traditional welding, with little to no post-weld finishing. In high-volume production, that speed is the core reason companies make the switch.
The Bottom Line
A laser welder and a MIG welder are answers to different questions. MIG is the forgiving generalist. Laser is the fast, precise specialist. Neither is “better” — each is correct in its own scene.
The beginner in that Reddit thread was asking the wrong question, and dozens of experienced welders told him so. If you’re welding thin stainless in a production environment and fighting labor costs and finishing time, you’re asking the right question — and a laser may well be the right answer.
Ready to see what a laser welder can do on your material, in your shop? Tell us what you’re welding and we’ll run a free sample weld test on your actual parts — no obligation, just proof.
Other post you might like
Handheld Laser Welder Safety: The Honest Guide
A few months ago, someone on r/Welding posted a short, worried note about handheld laser welder safety. His shop had